Categories
Latest blog
How Can Importers Ensure Quality When Sourcing Industrial American Type Light Duty Casters Wholesale?
Sep 15 , 2026
You ensure quality by qualifying suppliers rigorously, verifying technical specifications, and inspecting goods before shipment. Wholesale volume magnifies every defect, so you must build quality into supplier selection rather than check it at the end. Industrial American Type Light Duty Casters must match US dimensional and load standards, not generic international equivalents.
Qualify suppliers with factory audits and sample testing to ensure quality.
Verify load ratings and safety factors to prevent failures and reduce liability.
Confirm US compliance and certifications to avoid costly import problems.
You must verify the load rating before placing a wholesale order. The rated load capacity represents the maximum weight each caster supports under normal operating conditions. Ask the supplier for test data that confirms the rating. A safety factor protects against sudden shock loads, uneven floor surfaces, or slight overloading during use. Industry practice recommends a minimum safety factor of 1.5 times the total expected load. For example, if your application requires 1,000 pounds of total support across four casters, each caster should carry a rated capacity of at least 375 pounds, not 250 pounds.
Request documentation that shows the test methodology. Reputable suppliers provide static load test reports and dynamic load test results. Dynamic testing simulates real-world movement conditions. Static testing measures the maximum weight before structural failure. You should also confirm that the load rating applies to the specific wheel material and mounting configuration you intend to use.
Always require a safety factor of at least 1.5x the total expected load. This standard protects your equipment and reduces liability risk.
Material selection directly impacts performance and longevity when you purchase Industrial American Type Light Duty Casters. The frame should use cold-rolled steel with a minimum thickness of 0.10 inches for light-duty applications. Zinc plating or powder coating provides corrosion resistance. For food or medical environments, you must follow stricter guidelines.
Pay close attention to wheel and bearing materials in these settings:
Wheel tread material must be non-porous, chemical-resistant, and free of leachable additives for food or medical environments.
Food-grade polyurethane should align with 21 CFR Part 177.
Thermoplastic rubber (TPR) and polypropylene meet FDA requirements for dry or mildly wet zones.
You should avoid standard industrial rubber, zinc-plated steel wheels, or materials without documented FDA compliance.
Lubricants require NSF H1 registration.
Sealed stainless steel ball bearings serve as the industry standard for washdown applications.
The construction method also matters. Insist on a double-weld process at the joint between the top plate and the horn. A single weld introduces a failure point. Check that the swivel bearing uses heat-treated raceways to prevent premature wear. These details separate a durable product from a disposable one.
You must confirm that the caster meets US dimensional standards, not generic international equivalents. The bolt hole pattern typically uses 2-5/8 inches by 3-5/8 inches spacing for light-duty top plates. Overall height and swivel radius must align with US specifications. Measure the actual dimensions against the supplier's data sheet before you approve samples.
For certification, request documented proof of US compliance. The table below summarizes key certification frameworks and the documentation you should request from your supplier.
| Certification Framework | Scope of Coverage | Documentation to Request |
|---|---|---|
| NSF/ANSI 2 & 51 | Design, materials, and finishes for food equipment | A verifiable NSF listing number rather than a self-declaration |
| FDA 21 CFR 174–178 | Indirect food additives, polymers used in wheel treads, and lubricants | Material declarations that cite the specific CFR sections |
| ISO 13485 (Clause 7.4) | Medical device purchasing controls at the OEM level | Supplier audits and documentation from caster vendors |
You cannot rely on a supplier's verbal assurance. Request the actual certification documents. Cross-check the listing number on the NSF website or the specific CFR section referenced in the material declaration. This step prevents costly compliance failures after your shipment arrives.
You cannot judge a supplier by their catalog or their price list. You must verify their capability through direct investigation. This section walks you through the three pillars of supplier qualification: factory audits, sample testing, and reference verification.
Factory Audits and Capability Checks
A factory audit reveals what a supplier's website cannot. You or your third-party inspector must visit the production floor and examine the actual conditions. Do not accept video tours or photo galleries as substitutes for a physical audit.
Start with the basics. Examine the production equipment, factory size, and quality control processes. Look for a detailed description of the manufacturing process at each station. Evaluate the machinery and testing processes the factory uses. A supplier who cannot explain their own production flow has something to hide.
Your audit checklist should cover these areas:
Vet the caster wheel supplier on manufacturing capability, quality control, certifications, and after-sales service.
Review material certificates, production process charts, and sample testing reports covering load tests, abrasion resistance, and temperature tolerance.
Evaluate total cost of ownership — wheel lifespan, floor wear, noise levels, and replacement frequency — rather than unit price alone. This is particularly critical when validating the specific performance claims of products like a PVC Furniture Casters Wear resistant Mute Wheels 360 Swivel Castor.
Establish clear technical specifications and acceptance criteria before placing a bulk order to avoid costly revisions later.
The audit must also confirm that the factory operates the right testing equipment. Ask whether the factory has a drum/rotation tester, static load tester, fatigue tester, and tensile (bond-strength) tester on-site. Request calibration records for each machine. Verify testing equipment and industry-standard tests such as load test, swivel and wheel rolling resistance test, brake test, and simulation tests. A factory without these tools cannot guarantee consistent quality.
Quality system and change control deserve special attention during your audit. Ask how the supplier ensures production lots match the approved sample. Their answer should cover incoming material checks, first-article inspection, in-process frequency, test sampling, nonconformance control, and final release records. Define what triggers reapproval — changes to wheel compound, raw-material supplier, bearing, bracket thickness, heat treatment, plating, tooling, or production site. A supplier without a formal change control process will eventually ship you a product that differs from your approved sample.
Pilot production verification separates serious suppliers from order-takers. Test the process, not just the product. Confirm work instructions, gauges, approved materials, traceability, and packaging are present at the intended production station. Inspect samples from the pilot lot, not hand-built prototypes. Resolve nonconformities through documented correction and repeat verification before scaling.
Your audit focus should also reflect your target market. Different regions demand different priorities:
| Target Market | Audit Focus Areas |
|---|---|
| Germany / wider Europe | Documentation, controlled specifications, corrosion performance |
| Brazil, Colombia, Peru | Robust export packing, clear Portuguese/Spanish labeling |
| Korea | Precise drawings, consistent finish |
| Saudi Arabia, Kenya | Heat, dust, storage, and shipping route concerns |
| Russia | Climate and logistics review |
These are planning prompts, not legal conclusions. You must confirm current local regulations, language, conformity, and customs requirements for your specific market.
Sample testing transforms a supplier's claims into measurable facts. You must test physical samples against your own load calculation and environmental conditions before committing to volume. Do not rely on the supplier's internal test data alone.
Begin with a clear load calculation. Required load per wheel = (cart's empty weight + maximum applied load) ÷ number of wheels. For a 4-wheel cart, the industry-standard practice divides the total load by 3, not 4, because uneven floors and load distribution mean not all four wheels bear equal weight simultaneously. A supplier whose quoted per-wheel rating assumes perfectly even 4-way load distribution is overstating real-world capacity.
Required load per wheel = (cart's empty weight + maximum applied load) ÷ number of wheels. For a 4-wheel cart, the industry-standard practice divides the total load by 3, not 4, because uneven floors and load distribution mean not all four wheels bear equal weight simultaneously. A supplier whose quoted per-wheel rating assumes perfectly even 4-way load distribution is overstating real-world capacity.
You should run several test types on your samples. Each test verifies a different performance dimension:
| Test Type | Verifies | OEM Risk If Skipped |
|---|---|---|
| Static load test | Max weight while stationary, no permanent deformation | Structural failure under stationary equipment |
| Dynamic/drum test (ISO 22881-22884) | Wear and obstacle-clearing performance over rated cycles | Premature wheel cracking or seizing in the field |
| Fatigue test | Repeated stress cycling without bearing or axle failure | Critical for continuously moving equipment like AGVs and carts |
| Tensile/bond test | Adhesion strength between tread and metal core | Tread delamination and separation failures |
For dynamic testing, follow a controlled protocol. Run casters on a hard, horizontal test floor fitted with obstacles sized to 2.5%–5% of wheel diameter. Softer treads under 90 Shore A use the larger obstacle; harder treads use the smaller. Maintain controlled ambient temperature of 59–82°F during testing. For medium/heavy-duty casters, complete 15,000 wheel rotations and clear 500 obstacles. Run in cycles of three minutes running by a one-minute break. Confirm no deformation that impairs function after completion.
The ISO 22881 standard applies directly to light-duty institutional casters. It specifies a test speed of 1.86 mph and an obstacle height of 3% of wheel diameter. Use this standard as your baseline for Industrial American Type Light Duty Casters. For heavier applications, ISO 22883 requires a test speed of 2.49 mph, 15,000 wheel rotations, and 500 obstacles. ISO 22884 covers heavy-duty casters at higher speeds up to 3.73–9.94 mph depending on class.
You should also conduct specific functional tests. Static load testing mounts the caster upside down on a thick ribbed plate. Apply load to the wheel in increments based on load capacity for one-minute intervals. Record notes at each increment. Continue testing to failure or machine maximum to determine the maximum recommended sustained load capacity rating. Drop testing verifies swivel functionality. Use a solid steel wheel, mount the caster to a test stand, and drop a 25 lb. weight onto the wheel starting at 1 ft. and increasing to 10 ft. or failure. Inspect the caster for function between drops and document results. Cart push/pull testing evaluates swivel capability and rolling resistance. A 500 lb. mild steel cart can be loaded up to 2000 lb. Attach the cart to an electric motor via an S-type load cell to measure resistance. Test the force needed to move the cart in both directions and the breakaway force needed to swivel casters from various positions, such as 90 degrees to the cart axis and opposing one another.
The C.F.T.M.A. test measures durability of swivel casters under load. Mount the caster to an adaptor plate. An air cylinder applies the maximum load rating for the caster and wheel combination. A table moves 4.5 ft. back and forth in a straight line underneath the wheel. The caster indexes 180 degrees at each reversal. One cycle equals one full 4.5 ft. movement in each direction. The machine runs at 17 cycles per minute for 8 hours or until failure. Examine the wheel and caster against quality parameters after the test.
Request the actual test report showing obstacle count, rotation cycles, and test speed used — not just a summary load figure. Obtain full CAD drawings, ISO-referenced test reports, and raw material certifications before committing to a first order. Push for a minimum one-year warranty in writing, with clauses covering specification tolerances, packaging, lead time, and warranty claim procedure.
Certifications provide independent proof of a supplier's claims. You must verify each certificate directly with the issuing body. Do not accept scanned copies at face value.
A reliable wholesale supplier should possess ISO 9001 certification. This international quality management system certification focuses on continuous improvement and customer satisfaction. It ensures consistent production quality across lots. Some suppliers may also hold IATF16949, which indicates automotive-grade quality controls. Request scanned ISO 9001, CE, RoHS, and (where relevant) NSF certificates with certificate numbers. Cross-check those numbers against the issuing body's public database.
The table below summarizes key certifications and their relevance to your sourcing decision:
| Certification | Description | Relevance to American Caster Manufacturers |
|---|---|---|
| ISO 9001 | International quality management system (QMS) certification focused on continuous improvement and customer satisfaction | Highly valued by customers; ensures consistent production quality |
| UL Certification | Underwriters Laboratories safety certification for the American market | Important in settings where mechanical mobility and electrical safety intersect (e.g., hospitals, medical equipment) |
| ANSI/ICWM Standards | Design and performance criteria established by the American National Standards Institute (ANSI) and the Institute of Caster and Wheel Manufacturers (ICWM) | Frequently met by commercial and industrial casters; covers rated load capacities and performance requirements |
| SGS Certification | Third-party inspection and verification for product quality by an independent testing company | Often requested as evidence of environmental compliance, material quality, and load-bearing capacity |
You should also verify material compliance certifications. Request REACH and RoHS documentation, regional material compliance certificates, and test reports from accredited laboratories. These documents confirm that the caster materials meet environmental and safety regulations in your target market.
Reference checks complete the qualification picture. Ask the supplier for contact information of three to five existing customers, preferably in your region or industry. Call these references and ask specific questions about product consistency, delivery reliability, and how the supplier handles quality problems. A supplier who hesitates to provide references has a reason for that hesitation.
Repeat-order monitoring should continue after your first purchase. Track incoming defects, field feedback, push-force drift, corrosion, brake issues, and packaging damage by model and lot. Review trends with the supplier as part of controlled learning rather than a one-time audit. This ongoing process catches problems before they reach your customers.
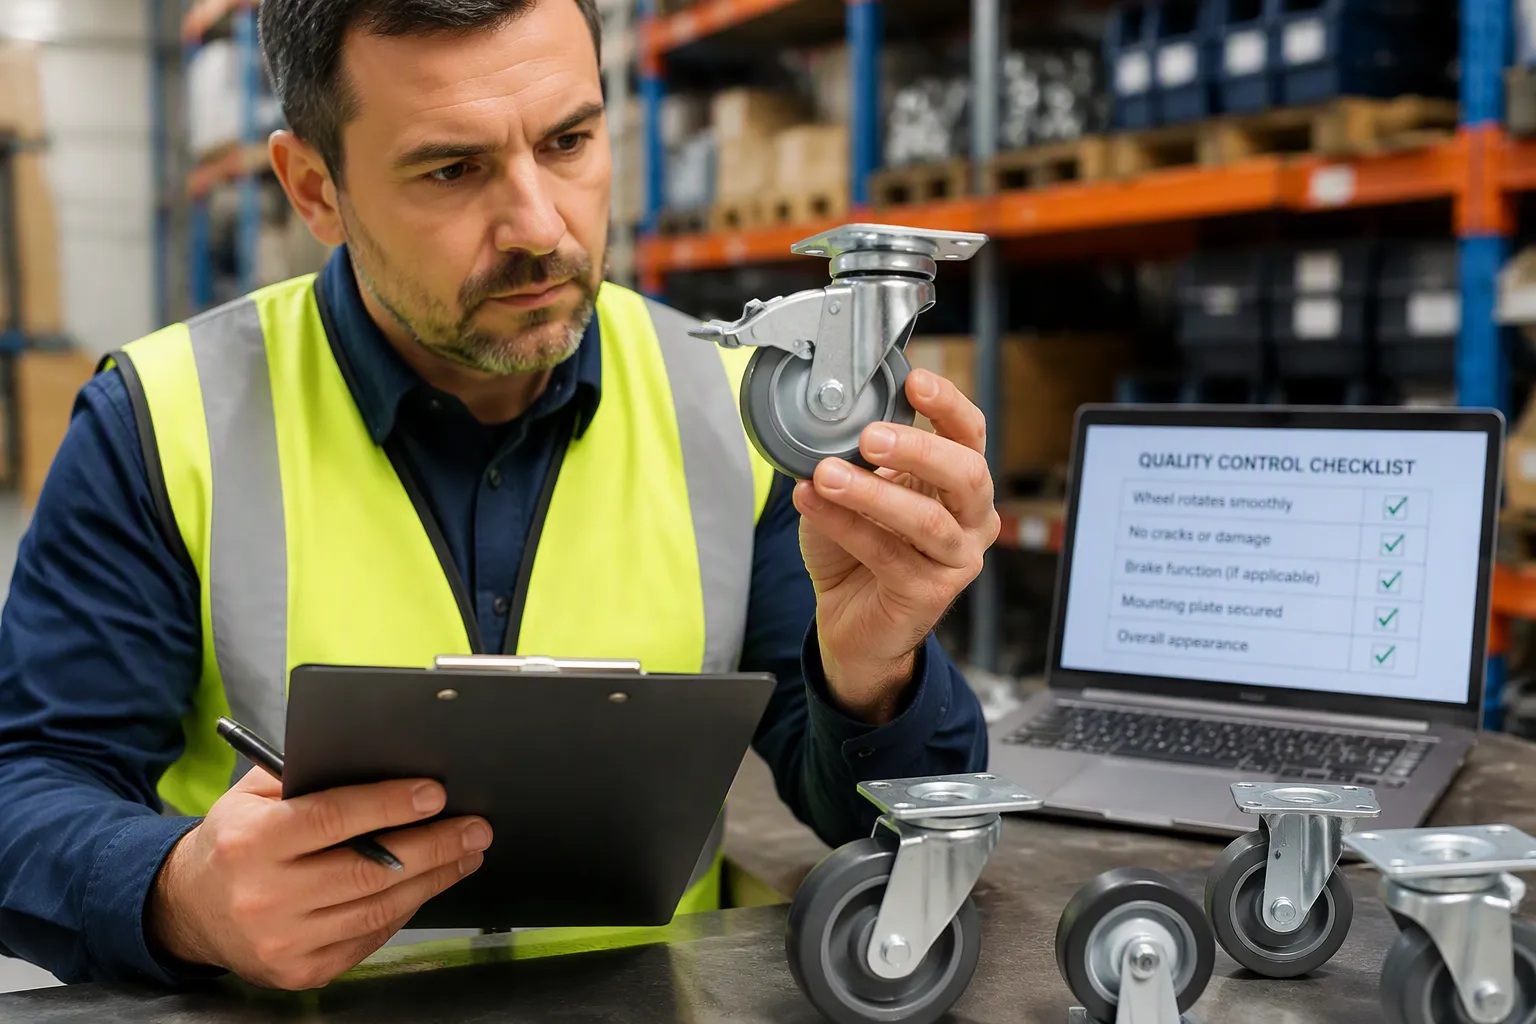
Pre-shipment and receipt checks form your final quality gate. Approve label content, photograph the packed pilot carton, and link carton labels to model and PO. Request final inspection evidence before shipment. On receipt, verify identity, dimensions, visible damage, wheel rotation, swivel, and brake function before releasing the lot. These steps protect you from accepting a shipment that fails to meet your specifications.
For Industrial American Type Light Duty Casters, you must separate static load capacity from dynamic load capacity. Static capacity measures the maximum weight while stationary. Dynamic capacity matters more and typically reaches only 60 to 75 percent of the static rating. Floor surface quality, travel speed, and transitions like expansion joints all reduce effective capacity.
| Load Type | Typical Rating Relationship | Key Influencing Factors |
|---|---|---|
| Static load capacity | Baseline rating | — |
| Dynamic load capacity | Typically 60–75% of static load rating | Floor surface quality, travel speed, floor transitions |
To verify claims, follow these steps. First, ask the manufacturer which specific test they performed, including load, speed, and obstacle conditions. Second, request an agreed test report for safety-critical applications. Third, perform an independent load-sharing calculation: divide total operating mass by three for a four-caster cart. Frame distortion signals exceeded load capacity. Inspect the bracket and top plate for bending before approving any batch.
The bearing system determines caster longevity.
Sealed ball bearings are what separate a commercial caster from a residential one. They prevent debris, water, and fine particles from entering the bearing race, which is what causes premature seizing.
Watch for these signs of substandard material quality:
Loss of tread depth exceeding 1mm, indicating replacement needed within 30 days
Radial cracks visible on the wheel surface
Irregular rotation patterns that signal bearing issues
Hardened rubber with Shore A hardness above 90
A 2023 study found 78% of seized casters had either single-shield bearings or zinc-plated steel races instead of stainless steel.
Verify that your supplier uses sealed stainless steel bearings for your Industrial American Type Light Duty Casters. Cheap bearings today create warranty claims tomorrow.
A perfect sample does not guarantee a perfect production run. Implement in-process inspections to catch variation. Some manufacturers integrate impact testing with machine vision to detect cracks before further assembly.
To maintain consistency across your bulk order, implement these controls:
Create detailed inspection sheets specifying characteristics, frequency, and gauge tolerances
Classify defects as critical, major, or minor with defined acceptance levels
Pull random samples from production lots and record results
Tag and isolate non-conforming product with red reject tags
Implement a Corrective and Preventive Action (CAPA) process for recurring issues
Request batch-level end-of-line load test certification. This document confirms each production lot meets the promised performance. Pair it with load-versus-speed charts showing how capacity changes with operating speed.
Quality assurance for Industrial American Type Light Duty Casters starts with supplier qualification, not post-order inspection. Build your program on three pillars: verified specifications, audited suppliers, and contractual quality agreements. Request samples now, run load tests, and draft a quality assurance agreement with inspection clauses.
Request full CAD drawings, ISO-referenced load test reports, raw material certifications, and a written warranty. These documents confirm the supplier meets your specifications before production begins.
Ask for dynamic load test data, not just static ratings. Run your own load calculation by dividing total weight by three for a four-caster cart. Independent testing reveals the true capacity.
You must establish a formal change control process with your supplier. Define what triggers reapproval for materials, tooling, or production sites. In-process inspections catch variation before shipment.